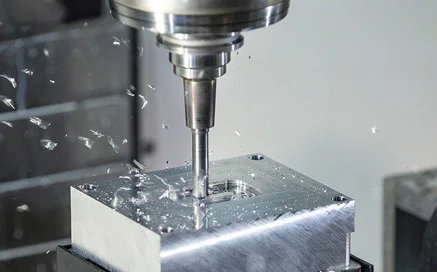

Holes might look like one of the simplest features in a part, but they can be tricky to machine because the cutting tool has to work inside a confined space, where access, chip removal, heat, and tool rigidity all become more difficult.
Design choices like depth, diameter, and placement can affect accuracy, machining time, and cost. Knowing the different types of CNC machining holes, and when to use each one, makes it easier to design parts that do what you need without adding unnecessary complexity. Here is an overview of the most common hole types, practical design tips, and a few common mistakes to avoid.
At Konlida, our CNC machining services handle a wide range of hole features—from simple through holes to complex threaded and reamed holes—with automated DFM feedback to help you optimise your design before machining begins.
Common Types of CNC Machining Holes
Most engineers are familiar with holes—black holes and rabbit holes included—but there are a few more practical types worth knowing if you want to avoid tumbling down the metaphorical ones.
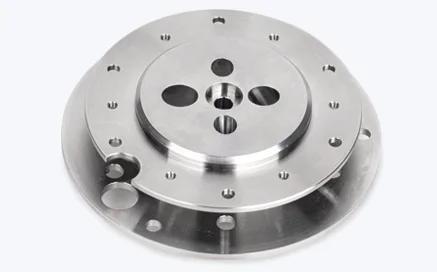
Some holes provide clearance for fasteners, while others align mating parts with locating pins, carry fluids, or create a threaded connection. And although we often talk about “drilling” holes, that is only one way to make them. Depending on the diameter, tolerance, material, and finish you need, a CNC hole might be drilled, interpolated with an end mill, or reamed.
Here are the most common types you will run into:
Through Holes
A through hole extends completely through the part. These are usually among the simplest holes to machine because the tool can pass all the way through and chips have somewhere to go. They are commonly used for clearance holes, alignment features, fluid or air passages, and weight reduction. If your design works just as well with a through hole as a blind one, the through hole is usually the easier option.
Blind Holes
A blind hole stops before reaching the opposite side of the part. That is useful when one surface needs to stay intact or when a through hole would interfere with another feature. The trade‑off is that chips cannot simply exit through the bottom, so machining takes a little more work. If you are designing a blind threaded feature, proper depth planning is essential.
Tapped (Threaded) Holes
Tapped holes contain internal threads so a screw or bolt can fasten directly into the part. Specify only the thread depth the connection needs, since extra depth can drive up machining time without really improving holding strength. At Konlida, internal threads are cut with a thread mill rather than a traditional tap, allowing one tool to cut multiple thread sizes that share the same pitch and reducing setup time.
For detailed guidance on thread types, depths, and manufacturability, see our threading options for CNC machining .
Counterbore Holes
A counterbore adds a larger cylindrical recess above a smaller hole. This lets socket‑head cap screws and similar fasteners sit flush with or below the part surface, so the head does not stick out or interfere with other components.
Countersink Holes
A countersink uses a conical recess instead of a cylindrical one. It is designed for flat‑head screws that need to sit flush with the surrounding surface. Just make sure the angle matches the fastener you are using, since common standards include 82°, 90°, and 100°.
Reamed Holes
A reamed hole comes into play when a standard machined hole is not accurate or smooth enough. The hole is made slightly undersized first, then a reamer removes a small amount of material to bring it to its final size. Reamed holes are often used for dowel pins, precision shafts, bearings, and alignment features. Keep in mind that reaming adds another operation, so only use it when you need that level of precision.
Best Practices for Designing Holes in Machined Parts
A few practical design choices can make it a whole lot easier to machine holes while helping control cost and accuracy.
Drill Sizes
Generally, it is a good idea to choose standard hole and fastener sizes when they meet your requirements, since added complexity can bloat your budget and stretch your schedule. At Konlida, however, most milled holes are interpolated with an end mill, so engineers can specify the diameter their design needs.
Hole Diameter and Depth
Deep holes are harder to machine because chips are more difficult to clear and longer tools are more likely to flex. Keep holes only as deep as needed, and use a through hole instead of a blind hole when the design allows.
For a comprehensive overview of CNC design principles—including hole depth optimisation and feature accessibility—see our guide to optimising CNC part design .
Tool Access
Holes inside deep pockets or close to tall walls may require longer, less rigid tools, which can hurt accuracy and increase machining time. Give the tool a clear path to the feature whenever possible.
Materials
Hole machining behaves differently depending on the material. Harder metals can increase tool wear, while some softer plastics can flex or deform, making it harder to maintain tight tolerances. For guidance on how different materials affect machining, see our 1018 vs. 4140 steel guide or aluminium alloy comparison .
Tolerances
Tighter tolerances take more time to machine and inspect. Reserve them for holes where fit is critical, such as bearings, dowel pins, or precision shafts.
For an in‑depth look at tolerance selection and GD&T, see our understanding CNC machining tolerances guide.
Edge Distance
Holes placed too close to an edge can weaken the part and make machining more difficult. When checking edge distance, consider the largest diameter of the entire feature, including counterbores and countersinks.
Chamfers
Use a chamfer to help guide screws, pins, or shafts into a hole. If you only need to remove a sharp edge, call for an edge break instead of tightly controlling the chamfer dimensions.
How to Choose the Right Hole Feature
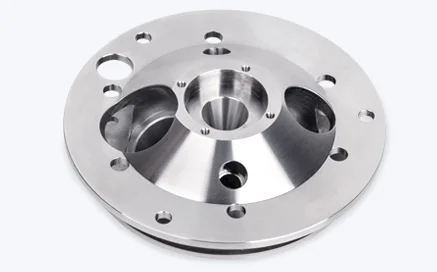
When choosing between hole features, consider the required fit, fastener type, available material thickness, tool access, and tolerance. In general, use the simplest feature that meets the functional requirements, since simpler hole designs are generally faster to machine and easier to inspect.
| If you need to… | Consider using… | Why |
|---|---|---|
| Pass a fastener through a part | Through hole | Usually the simplest option when the hole can extend through the part |
| Thread directly into the part | Tapped hole | Eliminates the need for a separate nut |
| Recess a socket‑head fastener | Counterbore | Lets the fastener head sit flush with or below the surface |
| Flush‑mount a flat‑head screw | Countersink | Matches the tapered head of the fastener |
| Achieve precise alignment | Reamed hole | Provides tighter diameter control and a smoother finish |
| Keep the opposite surface intact | Blind hole | Stops the hole before it passes through the part |
For more ways to improve manufacturability, see our design validation with SOLIDWORKS guide .
Common Mistakes to Avoid
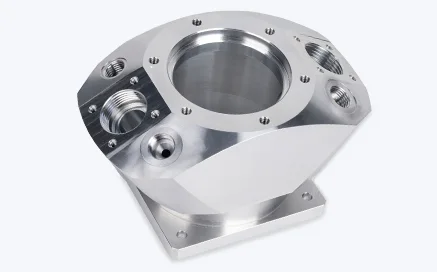
The most common issues when CNC machining holes come from adding more depth, precision, or complexity than the feature actually needs, or overlooking how the tool will reach and machine the hole.
Watch out for these pitfalls:
- Specifying unnecessarily deep blind holes
- Choosing non‑standard fastener sizes without a functional reason
- Applying tight tolerances to non‑critical features
- Positioning holes too close to part edges
- Forgetting to specify countersink angles
- Calling for unnecessary thread depth
- Designing features with poor tool access
When designing parts with complex hole features that require multiple set‑ups, understanding how jigs and fixtures can improve accuracy and repeatability is essential.
The choice between 3‑axis and 5‑axis machining also affects how holes can be accessed and machined. For an overview of these options, see our 3‑axis vs. 5‑axis machining guide .
Summary
| Hole Type | Best Use | Key Consideration |
|---|---|---|
| Through hole | Fastener clearance, fluid passages | Simplest option when possible |
| Blind hole | When opposite surface must remain intact | Chips cannot exit through bottom |
| Tapped hole | Threaded connections | Specify only necessary thread depth |
| Counterbore | Flush fastener heads | Allows cap screws to sit below surface |
| Countersink | Flat‑head screws | Match angle to fastener standard |
| Reamed hole | Precision alignment, dowel pins | Adds extra operation; use only when needed |
Ready to Start Your CNC Machining Project?
Konlida’s automated DFM analysis reviews your uploaded CAD model and flags hole features that may be difficult to manufacture—giving you a chance to optimise the design before machining begins.
FAQ
A through hole passes completely through the part. A blind hole stops at a specified depth.
Practical depth depends on diameter, material, tolerance, and access. Holes deeper than roughly six diameters deserve an early manufacturability check.
Use one when a pin, bearing, bushing, or shaft needs tighter diameter control and a smoother bore.
Yes, especially blind holes. The hole usually needs to extend deeper than the usable threads to leave room for the threading tool to finish its cut and for chips to collect below the threaded section.
A counterbore has straight walls and a flat seat. A countersink is conical and designed for a flat-head screw.